


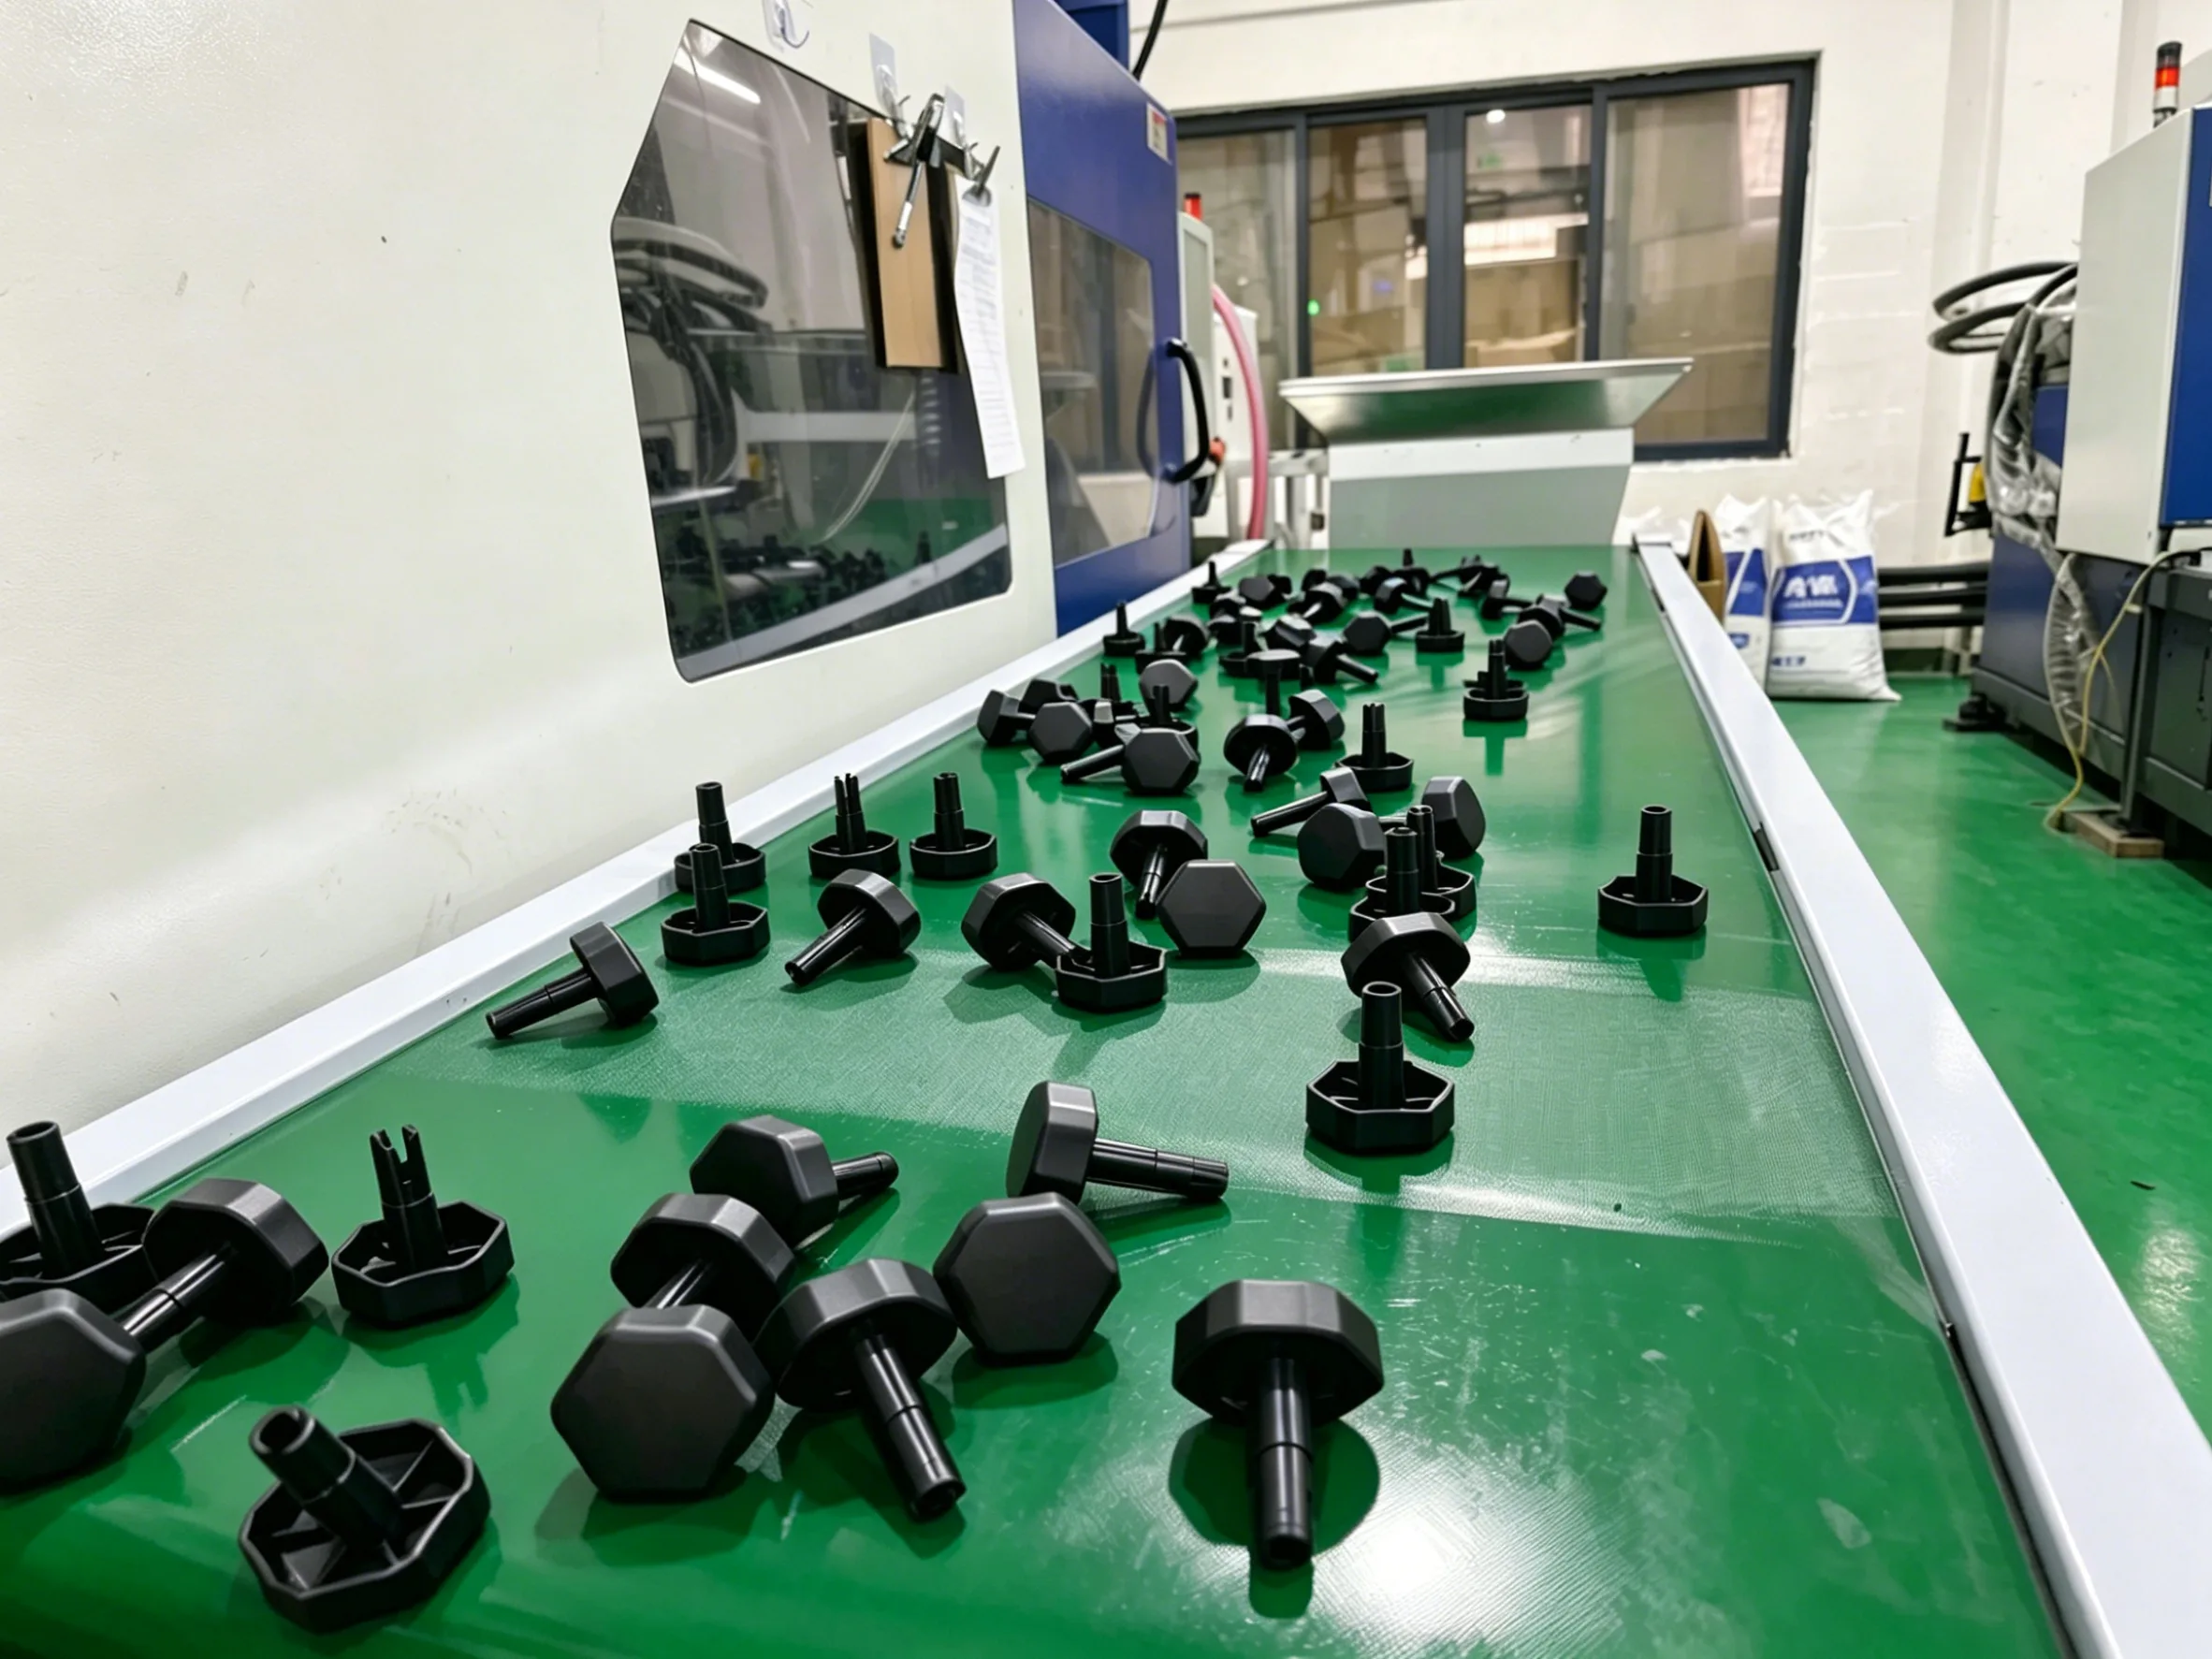
The most common culprit behind mass-production shrinkage is uneven wall thickness design. When molten plastic enters the cavity, the outer layer contacting the mold wall cools rapidly to form a solid skin. However, because plastics have poor thermal conductivity, the inner layer cools slowly to form a higher-density core—thicker walls mean slower cooling and greater overall shrinkage.
The catch is that during trial runs, extended holding times can temporarily mask this issue, allowing thick-walled sections to achieve adequate packing. But mass production demands efficiency, requiring cycle and cooling times to be compressed. Once holding time returns to normal parameters, insufficient cooling in thick sections triggers sink marks or even internal voids.
| Material Type | Crystallization Behavior | Shrinkage Characteristics | Typical Risks |
|---|---|---|---|
| Amorphous Plastics (ABS, PC, PMMA) | No crystallization; molecules freeze randomly | Lower shrinkage, less directional | High internal stress, cracking |
| Semi-Crystalline Plastics (PA66, POM, PET) | Molecules align into regular crystal lattices upon cooling | High shrinkage, highly directional (up to 40/1000+) | Sink holes, warpage, unstable dimensions |
Many product warpage issues in mass production stem from crystalline plastics. Represented by materials like PA66, POM, and PET, they exhibit a large density difference between molten and solid states, inherently driving high molding shrinkage. To complicate matters further, crystallinity is directly controlled by cooling rates:
During mass production, mold temperature distribution is rarely absolute uniform. Combined with aging cooling channels and mold temperature controller fluctuations, local crystallinity variations across the same batch can exceed 10%. This difference directly converts into internal stress—uniform shrinkage doesn't cause warpage, but uneven shrinkage does.
In a previous PET bottle base project, crystallinity variations at the wall-thickness transition zone caused ongoing internal stress release during storage, resulting in micro-cracks within two weeks. The root cause was abrupt shrinkage rate transitions triggered by uneven thickness.
From sampling to mass production, processing condition drifts can prove fatal:
| Critical Parameter | Recommended Control Range | Failure Consequence |
|---|---|---|
| Wall Thickness Uniformity | Adjacent wall ratio ≤ 1.5:1, rib thickness ≤ 60% of main wall | Sink marks, voids, warpage |
| Crystalline Mold Temp Fluctuation | ≤ ±3°C | Crystallinity variation → unstable dimensions |
| V/P Switchover Repeatability | ≤ 0.1 mm | Packing volume fluctuation → sink marks |
| Cooling Time | No less than 90% of trial-confirmed value | Ejection distortion, post-shrinkage |
| Moving/Fixed Mold Temp Difference | ≤ 10°C | Differential thermal stress → warpage |
| Gate Weld Hardness Variance | Within HRC ±3 degrees | ~15% risk of secondary cracking within 20k cycles |
🏭 DAQIDA Factory Qualification Certificates & Injection Molding Expertise
As a professional direct source factory, DAQIDA masters advanced plastic injection molding processes, DFM optimization, and strict production discipline backed by our official qualification certificates:
• Explore our full manufacturing capabilities via the DAQIDA Product Catalog ➔
Avoid common mass-production pitfalls like shrinkage and warping. Partner with DAQIDA for professional OEM and ODM manufacturing solutions built on precise DFM analysis, stable process control, and rigorous factory quality standards.
No account yet?
Create an Account